Core Design
Custom Nanocrystalline Cores Manufacturer: Qualifying a Supplier from Spec to Production (2026)
Who this guide is for
- • Power electronics engineers and magnetics designers choosing a custom nanocrystalline cores manufacturer
- • Sourcing and quality teams locking origin, lot-test language, and lead time
- • CMC, CT, RCD, EV OBC / charger, and 20–100 kHz transformer programs that catalogs do not cover
What you will leave with
- • A 5-stage qualification framework you can put on a supplier scorecard
- • The real production sequence (ribbon, wind, field anneal, finish, test), not a generic lamination story
- • Clear next steps: RFQ template, spec guide, and a quote against enforceable test conditions
A custom nanocrystalline cores manufacturer is qualified on process, not on a catalog μ number. The core’s permeability window, loss at the real (B, f, T) point, field anneal, finish, and handling decide whether a common-mode choke, current transformer, RCD sensor, or mid-frequency transformer meets EMC, accuracy, and thermal limits in the enclosure.
Nanocrystalline starts as melt-spun Fe-based ribbon (typical FINEMET-class chemistry: Fe–Si–B–Nb–Cu), rapid-solidified in the roughly 18–35 μm commercial thickness class, wound to shape, then magnetic-field annealed. That anneal, not the winding alone, sets μ, loss, and B-H loop shape. After crystallization the material is high-performance and brittle. A small error in ribbon class, anneal, coating stress, or lot-test language shows up as saturation under imbalance or DC, excess loss, or field failures that a dimensional check will not catch.
In 2026 the same audit has to cover origin and queue. Our supply-chain analysis documents how ribbon is concentrated in a few melt-spinning mills, and how custom lead times can move from a normal 12-week class into 22 weeks when a mill goes offline. Qualifying a manufacturer means confirming they can build the RFQ and that they will not park your line on that worst-case clock.
Choose your path
Leads nanocrystalline core material selection, custom geometry qualification, magnetic acceptance testing, and manufacturing-aware design workflows (including CoreMagna AI). IEEE member; focuses on EV, EMI, metering, and industrial power magnetics. See the full author profile.
Published August 21, 2026 · Technically reviewed August 2026 by Manoj Kumar, Chief Technologist · Anneal and test language aligned with the custom-core RFQ guide · ~16 min read
How this relates to the spec guide
This article is how to judge whether a manufacturer can build your custom core at volume, with repeatable lots. The companion specification article is how to write the purchase-ready RFQ: μ / AL test conditions, R / Z / F loop, drawings, and acceptance tests. Download the RFQ template before you send a competitor datasheet and ask for “equivalent.”
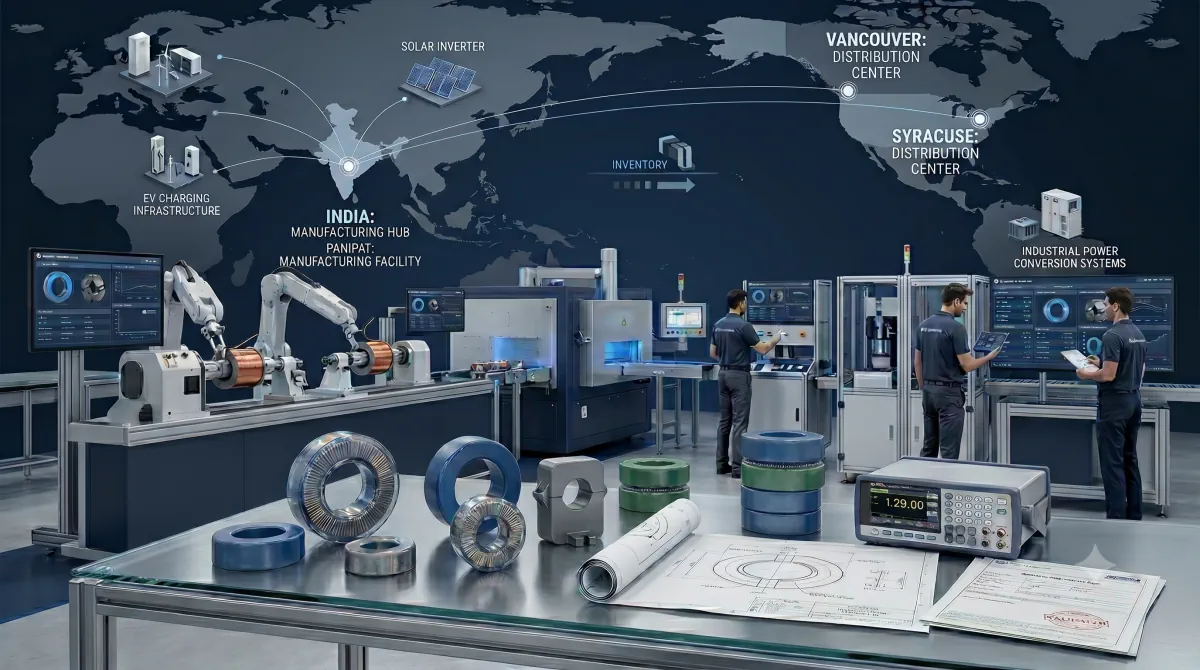
CenturaCores manufactures nanocrystalline, amorphous, and CRGO cores in Panipat, Haryana, India, with distribution in Langley, BC and Syracuse, NY. Spherical Insights has listed Centura Cores Inc. among key global players in nanocrystalline toroidal cores, alongside Proterial (formerly Hitachi Metals), VACUUMSCHMELZE, and Magnetec. That list is market context. The five stages below are the actual gate.
1. Technical and material capability audit
Audit ribbon quality and field anneal before you count machines. Floor space does not rescue a mill cert you cannot read or a furnace recipe you cannot hit.
1.1 Ribbon: source, class, and stacking
Most core houses buy precursor ribbon from a handful of melt-spinners; a winding plant is not a $50 million melt line. Ask the core vendor for mill name, grade family, incoming inspection, and lot certs. Laser gauging during melt-spinning belongs to the mill, not to the winder.
| Ask the core manufacturer | Why it matters |
|---|---|
| Ribbon source (mill and grade family) and country of origin | Dual-source and tariff paperwork; see China vs India |
| Thickness class (typical commercial 18–35 μm) and incoming inspection | Eddy-current loss scales with thickness, B, waveform, and T |
| Width, lot certs, chemistry as mill documentation | Homogeneity and crystallization behavior |
| Measured stack factor on the finished part | Sets Ae, not material Bs |
Thickness is a class, not a law. Plenty of 50–100 kHz designs still run 20–25 μm ribbon. Move to a thinner class (often 18 μm or below) only when measured loss or temperature rise crowds the budget. Failing a vendor because every core above 50 kHz is not 14–18 μm is the wrong audit.
For preliminary sizing we use Kstack = 0.75–0.85 on typical epoxy-impregnated toroids, unless the finished part has been measured. Do not assume 1.0. Stack factor changes Ae (volt-seconds and AL), not published Bs, which sits near 1.2–1.25 T at 25 °C for common Fe-based grades. A value under 0.75 is not automatic proof of rough ribbon; impregnation and geometry move it too.
Skip locking the PO to Fe73.5Si13.5B9Nb3Cu1 unless that exact mill grade is on the order. Name the alloy family, then freeze mill certs and electrical acceptance.
In recent CMC qualification reviews, the most common missing PO item has been the test condition for AL, not the nominal AL target. A window such as AL ≥ 60 µH/T² at 10 kHz, 0.1 A/m, 25 °C is quoteable. “AL = 60” with no frequency, field, or temperature is not.
1.2 Field anneal: specify R / Z / F with physics, not a letter
Loop letters are CenturaCores RFQ shorthand, not an IEC/IEEE standard. Pair the letter with remanence, anneal orientation, and DC-bias or pulse behavior.
| Loop (RFQ shorthand) | Character | Typical use |
|---|---|---|
| R-loop (round) | Lower remanence, softer knee, low loss | Power magnetics, many filters, general HF |
| Z-loop (square) | High remanence / squareness | Pulse, switching, some specialized sensors |
| F-loop (flat) | Transverse-field anneal; low remanence (Br / Bs < 10%); μ more stable under DC | Unbuffered CMCs, power inductors with DC, bias-tolerant EMI |
High-μ CMC, CT, and RCD work often starts in the ~80k–120k μi band and above, under the agreed test conditions. With DC or strong imbalance, specify F-loop and a Br / Bs limit; do not treat “zero-field, maximum μ” as a universal CMC rule. Gapped power and PFC-class parts often land near 5k–20k effective μ because the gap sets μe.
Effective permeability with a gap
Verify the vendor can run the anneal you will put on the PO, and that furnace capacity is sized for your volume. Anneal queue is often the lead-time bottleneck.
1.3 Geometry and finish they can actually freeze
CenturaCores has produced 5,000+ unique custom designs: toroid, oval, rectangular, C/cut, E, and bar, many from customer drawings. Envelope limits belong on the drawing review, not as borrowed slogans. The coated-toroid example below is the usual miss: the winding window was quoted on bare ID.
Freeze OD/ID/HT (or A/B/C) before and after coating or case, min ID after case, gap and mating flatness on cut cores, clamp-force limits, and finish (bare, epoxy, varnish, PBT case, stainless band). Post-anneal cores are brittle, so packing is part of the magnetic spec. See specialized packaging.
2. Prototype and first article inspection (FAI)
First article has to be tested at the flux, frequency, and temperature the circuit actually sees. A 25 °C LCR μ is useful incoming data. It is not FAI. Use an LCR meter for μ and AL under stated conditions; use a BH analyzer or power analyzer for core loss.
| Measurement | Instrument / method | Spec as |
|---|---|---|
| μ or AL | LCR or agreed fixture at stated f, H (or B), T | Window, not a single marketing μ |
| Core loss Pfe | BH analyzer or power analyzer on defined excitation; IEC 60404-aligned method as agreed | Loss at the real (B, f, T) point, including waveform |
| DC-bias / imbalance | μ or L vs H (A/m) or vs ΔI | Required L or Zcm at peak current or imbalance |
| Dimensions | After-finish CMM or gauges vs drawing | Max OD / min ID after case |
| Cut gap (if any) | Gap length, flatness | Locked g |
| Finish / case | Visual + mechanical; polymer flammability if claimed | PBT/PA66 UL 94 V-0 is a plastic rating, not a metal rating |
| Temperature | Repeat μ/loss at min/max ambient (typical product range −40 °C to +130 °C; high-temp versions to +155 °C) | Do not ask for Bs “stable to Tc ≈ 570 °C.” Bs falls with T |
Above about 50–100 kHz, eddy-current loss climbs with ribbon thickness, flux, waveform, and temperature. Put that loss number on the PO, then screen geometry in the Nanocrystalline Core Analyzer and custom core designer. Confirm on the bench.
Close FAI against the purchase-order conditions, not a generic certificate of conformity. If the RFQ is still thin, fill the template first. I still see first articles signed off on a 25 °C LCR sweep while the magnetics team is designing to 65 kHz and 100 °C. Those two tests are not interchangeable.
What we have seen in qualification
Stage 1 and Stage 2 exist because of programs like these. Details that would identify the OEM or the incumbent vendor are omitted.
FAI passed inductance, then failed loss at operating flux
A mid-frequency power core (roughly 40–60 kHz class) cleared first article on AL at a low-excitation LCR point. Incoming inspection looked green. On the converter bench the core ran hot. Loss at the converter’s actual flux, frequency, and temperature sat well above the thermal budget, even though 25 °C inductance was inside the PO window.
The PO had never named a loss method, waveform, or temperature. The vendor’s factory test was LCR-only. We rewrote acceptance to include BH-analyzer / power-analyzer loss at the operating point and a ribbon-class note when eddy current approached the budget. The next article passed electrically and thermally. The first lot would have shipped if we had treated inductance as a complete FAI.
Coated toroid whose finished ID stopped assembly
A cased CMC toroid was quoted and FAI-dimensioned to the bare ID on the customer drawing. Epoxy plus a PBT case ate enough radial build that the winding shuttle and insulation stack no longer cleared. Magnetically the part was in spec. Mechanically it would not assemble.
The drawing now freezes max OD and min ID after finish, with a note that coating thickness is process-controlled, not a suggestion. That is the same trap listed in Stage 1: after-case ID is part of the magnetic component, not a cosmetic extra.
3. Quality system and process control
Batch-to-batch μ is an anneal-and-handling problem as much as a QMS logo problem.
Plant baseline at CenturaCores is ISO 9001:2015 and ISO 14001, with IEC 60076 / IEEE C57 context on transformer programs and RoHS / REACH on materials. IATF 16949, AEC-Q200, and PPAP belong on automotive parts. They are not a blanket filter for every industrial CMC, and they are not automatic on every nanocrystalline line in a factory.
- Incoming ribbon: mill certs, thickness class, lot hold/release
- Anneal: recipe control, furnace logs, thermocouple/field records
- SPC on the parameters you actually buy: AL or μ at stated conditions, dimensions, mass, coating/case thickness
- Electrical test: 100% or skip-lot as written on the PO (AL / μ; loss or CT excitation when the design needs it). Q and leakage current belong on wound components, not on bare cores.
- Traceability: ribbon melt/lot → anneal run → finish lot → shipper
- Handling: post-anneal crack/stress rules; export pack-out
Ask for lot data from a similar geometry. A glossy quality brochure is not a substitute.
4. Supply-chain and lead-time risk
Ribbon production is the structural bottleneck (few mills, niobium, melt-spinning capital). Core plants then add slit, wind, anneal, finish, and test. Qualification without origin and queue is incomplete.
| Risk | Vulnerability | What qualified looks like |
|---|---|---|
| Upstream ribbon | Single mill, no certs, no alternate grade family | Named mill(s), lot certs, documented alternate |
| Anneal capacity | Tight μ window, no stated test conditions | Recipe + test conditions that can be hit without endless re-anneal |
| Custom case tooling | 6+ weeks for a one-off PBT tool | Standard cases first; custom tool only when the envelope requires it |
| Finished-goods clock | Make-to-order only, 12–22 weeks in a crunch | Stated custom queue and buffer (stocked sizes, regional DC) |
| Origin / tariff | Undocumented country of origin | COO paperwork; dual-region qualification if the program needs it |
Published CenturaCores clocks: 2–4 weeks on standard or stocked parts, 4–8 weeks on custom depending on complexity and anneal. International custom geometries have historically run 12–20 weeks, and 22 weeks in mill-outage crunches. Langley and Syracuse inventory exists so repeat sizes are not stuck on that clock. Local prototyping in British Columbia is being added to shorten concept-to-FAI for regional OEMs.
Questions for sourcing (ask; do not assume)
- Which melt-spinner supplies the ribbon, and is there a documented alternate grade?
- What is the anneal queue for this loop type and size, not a generic “4 weeks”?
- Custom housing: new injection tool vs a standard PBT/epoxy envelope?
- Can they hold finished or work-in-process buffer under agreed VMI/consignment, and at which process step? Un-annealed wound buffer only helps if anneal capacity is actually reserved; anneal is still the bottleneck.
- What packing standard protects brittle post-anneal cores on the lane you will use?
5. Scale-up and change control
After FAI, freeze the process before the volume purchase order.
| Gate | What to lock |
|---|---|
| Pilot | Capability on AL / μ and dimensions at PO conditions. If you require Cpk (for example ≥ 1.33 industrial, ≥ 1.67 automotive), write the characteristic and test method into the quality agreement. Pilot quantity should match the program, not a theatrical 1,000–5,000 piece run for a 200-piece job. |
| Traceability | Lot identity from ribbon through anneal to shipment. Laser etch on every core is a requirement to negotiate, not a universal industry default. |
| Process change (PCN) | Written notice (many OEMs use 90 days) for mill/grade, anneal recipe, or site change |
| Ongoing tests | Same test conditions as the PO; do not let production drift to a convenient LCR point |
| Packaging | Same pack-out as FAI; change of foam/tray is a magnetic risk |
CoreMagna AI can screen geometry, waveform-conditioned loss, and grade before you cut tools. It does not replace FAI measurements.
Qualification scorecard
A manufacturer that cannot answer these in writing is not ready for custom production.
- Will they quote μ or AL under stated (B, f, T) conditions?
- Can they run R, Z, or F anneal as specified, with a Br/Bs ratio or DC-bias limit written on the PO?
- Do they buy ribbon from a named mill and inspect thickness class, or only “high μ material”?
- Is FAI loss measured with a loss method, not an LCR meter?
- Are ISO 9001 (and IATF/PPAP if automotive) matched to this part, not to a different line?
- What is the anneal-limited lead time, and where is buffer held?
- Will lot data and PCN sit in the quality agreement?
Frequently asked questions
What should a custom nanocrystalline cores manufacturer prove in audit?
Named ribbon source and thickness class, field-anneal control for the R/Z/F loop on the RFQ, drawings with after-finish dimensions, electrical tests at purchase-order conditions, and a lead-time story that includes anneal queue and packing of brittle post-anneal cores.
Can nanocrystalline cores be made in custom shapes?
Yes. Toroid, oval, rectangular, C/cut, E, and bar are production geometries. Custom usually means a drawing-driven OD/ID/HT or A/B/C, a defined gap, a specified loop/anneal, and a finish that survives shipping. Stacked builds increase effective cross-section when a single oversized wound core is impractical.
What certifications should a custom nanocrystalline cores manufacturer hold?
ISO 9001:2015 and ISO 14001 as plant baseline, plus lot-test data matched to the purchase order. IATF 16949, AEC-Q200, and PPAP apply when the part is on an automotive path. UL 94 V-0 applies to plastic cases, not the metal core.
How do I choose between amorphous and nanocrystalline cores?
The choice depends on frequency, loss budget, size, and cost. Nanocrystalline offers high permeability and low loss in compact CMC, CT, RCD, or mid-frequency designs, with typical Bs of about 1.2–1.25 T at 25 °C. Amorphous remains practical for many power and cut-core transformer jobs. Compare datasheet values at the operating (B, f, T) point.
How long does custom nanocrystalline core production take?
At CenturaCores, standard stocked parts are typically 2–4 weeks and custom designs are typically 4–8 weeks depending on complexity and anneal capacity. International custom geometries have historically run 12–20 weeks, and 22 weeks during mill-outage crunches. North American distribution in Langley, BC and Syracuse, NY is used so repeat sizes are not stuck on that longer clock.
What does CenturaCores need to quote a custom nanocrystalline core?
Function; operating B or V·s, f, T; enforceable μ/AL test conditions; loop type (R/Z/F plus remanence or anneal requirements); dimensioned drawing; finish/gap; ribbon thickness class when HF loss matters; acceptance tests; quantity; and lead time. Start with the RFQ template or request a quote.
Next steps
- Fill the RFQ (conditions, loop, drawing, tests).
- Run Stages 1–4 against the incumbent and the alternate.
- FAI at the operating point, then freeze PCN and lot data before volume.
Engineering tools: Core Analyzer, Turns & Core Selection Calculator, custom designer, CoreMagna AI. Technical sales: contact.
Request a custom quote
Send the RFQ block and drawing for a buildable custom core quote.
Request Quote